Custom Turnkey Complete Cleanrooms for Precision Manufacturing
2026-09-11
In precision manufacturing, even a single airborne particle can compromise an entire production run. Yet most cleanroom providers offer generic solutions that force you to adapt your process to their design—not the other way around. That is why GENO Pharmatech approaches every project differently: custom turnkey complete cleanrooms built around your exact contamination control needs, from initial concept to final validation. No off-the-shelf compromises. No hidden integration gaps. Just a controlled environment engineered to protect your most sensitive operations. Here is what makes a truly custom cleanroom work—and why it matters more than you think.
Your Process Sets the Spec, Not Our Catalog
We don't hand you a catalog and ask you to pick the closest match. Instead, we start with your production line, your tolerances, your material handling, and the exact moment a part enters your workflow. That brief—your process—is the real specification. From there, our engineers reverse the usual question. It's not what do we already make, but what does your line demand.
This flips the typical vendor relationship. You won't be forced into a standard size, a near-enough alloy, or a finish that almost works. If your operation calls for a nonstandard thread, a specific hardness gradient, or a shape that doesn't exist in anyone's stock list, that's the starting point—not a special request buried in footnotes. The result is a component that drops into your process without forcing you to alter it.
That's why our engineering conversations begin with your process flow, not a product sheet. It keeps surprises off your floor, shortens the trial loop, and removes the quiet costs of adapting someone else's standard to a job it was never designed for.
The Material Science Behind a Contamination-Free Floor
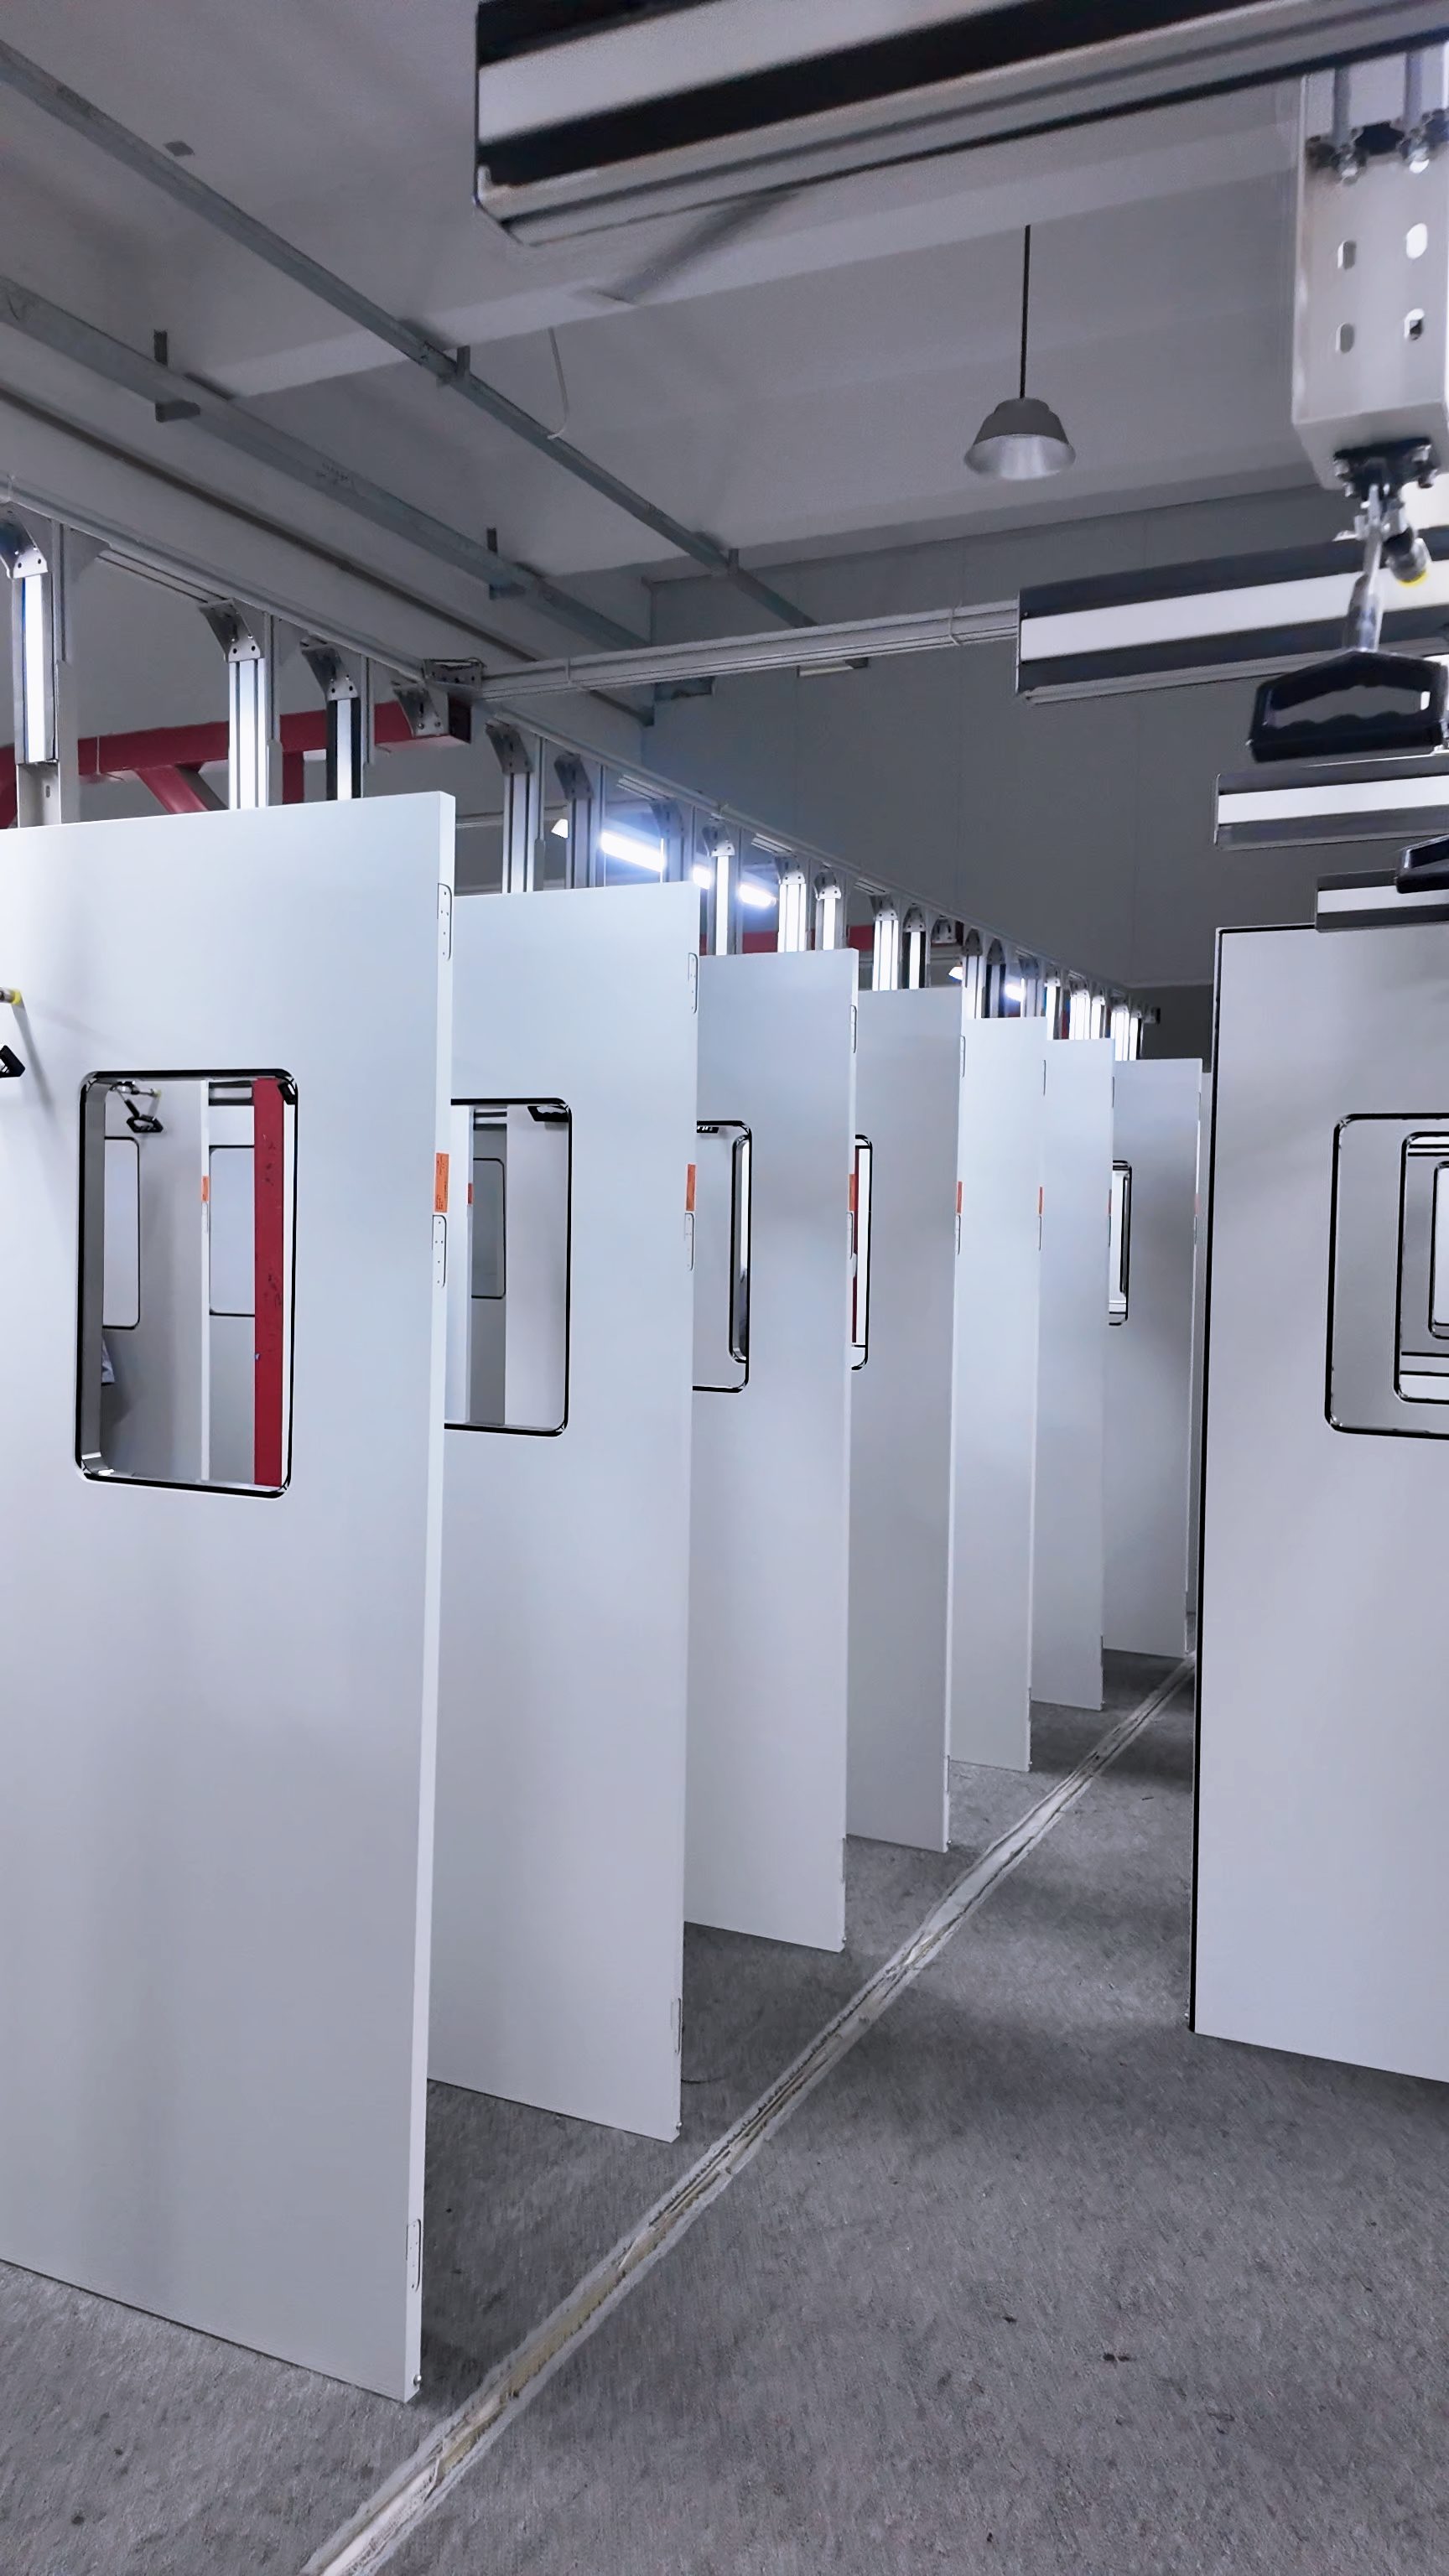
Contamination control in cleanrooms and critical manufacturing environments often focuses on airflow, filtration, and gowning protocols, but the floor itself is a surprisingly active participant. The material science behind a contamination-free floor hinges on selecting polymers, ceramics, or coatings with low particle shedding, minimal outgassing, and resistance to chemical attack. For instance, epoxy and polyurethane systems are favored because they cure into dense, non-porous surfaces that don't generate dust under foot traffic or wheeled carts. In contrast, ordinary vinyl tiles or concrete can micro-fracture and release fine particles over time, defeating even the best HEPA filtration.
Surface energy also plays a subtle but critical role. A floor with high surface energy tends to attract and hold airborne contaminants, while a properly engineered low-energy surface can reduce particle adhesion, making it easier to remove debris during wet or dry cleaning. Additives such as carbon nanotubes or graphene in conductive flooring don't just dissipate static electricity—they also alter the polymer matrix to improve abrasion resistance and reduce micropitting. This dual function is essential in electronics assembly, where a single microscopic particle can short a circuit.
Finally, thermal expansion coefficients and substrate bonding determine long-term integrity. If the floor material expands or contracts at a different rate than the concrete slab beneath it, hairline cracks can form at the interface, creating hidden reservoirs for bacteria or chemical residues. Advanced urethane cement systems are engineered to match substrate movement while remaining impervious to aggressive cleaning agents like hydrogen peroxide or quaternary ammonium compounds. Together, these material choices transform the floor from a passive surface into an active line of defense against contamination.
ISO Class Compliance Without the Guesswork
Cleanroom classification often gets reduced to a numbers game — particle counts, air changes, filter coverage — but compliance is rarely that neat. The real challenge isn't hitting a target; it's knowing which target applies to your process, your materials, and your people on any given shift. Without that clarity, teams either over-engineer the space and burn budget, or under-validate it and expose products to risk. The guesswork comes from treating ISO classes as interchangeable badges rather than as operational envelopes tied to specific activities.
A more grounded approach starts with mapping actual contamination sources: gowning friction, equipment exhaust, packaging tear, even the cadence of door openings. When you measure those inputs against your target class, you stop chasing arbitrary limits and start designing controls that matter. For instance, a Class 7 area might pass static particle tests yet fail during material transfer simply because the airflow pattern was never verified under dynamic conditions. Compliance, then, isn't a certificate on the wall — it's the confidence that your environment behaves predictably when it matters.
The shift away from guesswork also means treating ISO classes as a range, not a single number. Different operations within the same room can demand different states of control: a filling line may require Class 5 at the point of fill, while adjacent staging areas can operate at Class 7 without compromising sterility. By aligning classification with risk rather than with square footage, you avoid both the cost of over-classification and the hazard of false assurance. In the end, the goal isn't to impress an auditor with a lower number — it's to know exactly why that number holds up when your process is running, not just when the room is empty.
One Contract, Zero Blame Games: The Turnkey Difference
When a project is handed off piecemeal, every gap between vendors becomes a battlefield for finger-pointing. One team blames the foundation, another points at the wiring, and you’re stuck in the middle coordinating excuses instead of progress. That’s the hidden cost of assembly-line contracting: the more hands involved, the easier it is for each one to claim the other dropped the ball.
A turnkey approach flips this dynamic. You hire one partner who takes responsibility for the entire outcome, from the first blueprint to the final walkthrough. There’s no room for blame games because there’s only one phone number to call. If a cabinet arrives scratched or a timeline slips, the turnkey contractor owns the fix—not just the sympathy. That single point of accountability changes the entire energy of a project.
In practice, this means you stop being a referee and start being a client again. Decisions get made faster, because the team planning the schedule is the same team pouring the concrete and pulling the permits. When everyone answers to the same boss, coordination stops being a hope and becomes a built-in habit. The result isn’t just a finished space—it’s a process where every detail was someone’s responsibility, not someone else’s problem.
Why a Custom Cleanroom Pays for Itself Faster Than You Think
The upfront price tag on a custom cleanroom often triggers sticker shock, but that reaction misses how quickly the right design eliminates waste you didn't even know you were paying for. When engineers tailor air change rates, filtration placement, and material finishes to your exact process instead of forcing a generic Class 100 room onto a job that only needs ISO 7 in one corner, you stop burning money on over-specification. Every unnecessary HEPA filter, oversized air handler, or extra pass-through chamber silently drains your budget for years. A custom build cuts those elements out from day one, and the savings start compounding immediately.
Operational costs tell an even sharper story. A well-designed custom cleanroom reduces energy consumption by aligning pressurization cascades and humidity control with your actual production schedule rather than running full tilt around the clock. Lower fan speeds, smarter sensor placement, and easier access for filter changes translate into fewer technician hours and less unplanned downtime. Over a typical five-year span, those reductions routinely add up to two or three times the initial cost difference between a custom solution and an off-the-shelf alternative that you would have had to retrofit anyway.
Then there is the hidden productivity factor. When a cleanroom fits your workflow, operators move through gowning, material transfer, and equipment access without fighting cramped layouts or awkward air returns. Contamination events drop because the airflow actually protects the product rather than just satisfying a certificate. Fewer rejected batches and less rework mean the room pays for itself not through accounting tricks but through the simple math of more good units out the door every month. Most companies find the break-even point lands well inside the first year—often before the final commissioning report is even signed.
Precision Manufacturing Demands More Than Just a Clean Room
A certified clean room keeps particle counts low, but that alone won’t hold tolerances when a temperature drift of half a degree expands a wafer or a passing forklift sends vibration through the floor. Precision manufacturing lives in the nanoscale, where thermal expansion, acoustic noise, and structural micro-motion all compete with your process. You can have the best filtration in the building and still scrap a batch because the air handling system creates a draft across a laser interferometer.
Static charge builds up on insulators faster than most cleanliness protocols address it. A stray electrostatic discharge won’t just damage sensitive electronics; it can pull particles out of laminar flow and pin them to surfaces that were just cleaned. Similarly, airborne molecular contaminants—outgassing from materials, trace amines from packaging—settle invisibly and change surface chemistry. A clean room with particle counters won’t flag these failures.
What actually separates repeatable precision from hopeful clean-room operation is the unglamorous work: mapping airflow for dead zones, isolating equipment from building vibration, monitoring humidity to keep photoresist stable, and training people to move without disrupting the environment. The room is a starting condition, not a guarantee. The manufacturing outcome depends on how well every subsystem—thermal, mechanical, electrical, and human—stays within a narrow window while the process runs.
FAQ
Everything from the raised floor to the ceiling grid, plus HVAC with HEPA/ULPA filtration, lighting, doors, windows, and controls. We also handle the architectural finishes, electrical, plumbing, and process utilities so you're not stuck coordinating six different contractors.
We start with your particle count target and work backwards. Air change rates, filter coverage, pressurization cascades, and gowning protocols are selected to hit that class without wasting energy. The room gets tested under real operating conditions, not just empty.
Yes, that's a core part of the design. We use modular wall systems where possible, keep utility chases accessible, and leave spare capacity in the air handling unit. Moving a wall or adding a pass-through later is much cheaper than rebuilding.
A typical small to mid-size cleanroom takes 3 to 5 months depending on site conditions and custom equipment lead times. If you need to hit a production deadline, we can phase the work or fast-track certain components, but that usually requires earlier decisions on finishes and MEP.
Yes, we bring in an independent testing firm for particle counts, airflow velocity, room pressurization, and filter integrity. You get a full documentation package with test reports and as-built drawings. We don't consider the job done until the room passes.
Mostly semiconductor, medical device, optics, and microelectronics assembly, but we've also done aerospace and pharmaceutical packaging. The common thread is tight tolerance manufacturing where a single particle can scrap a batch.
We design the HVAC around your equipment heat load and your tolerance band. Tight control might require chilled water coils with reheat, a dedicated dehumidification loop, or a desiccant wheel for very low dew points. Sensors feed back to a central controller with alarms.
Because the hard part isn't the panels, it's the interfaces. The HVAC has to work with the electrical and the process exhaust, the lighting can't interfere with sensitive optics, and the room has to pass certification. When one team owns those interfaces, you get a room that works the first time.
Conclusion
In precision manufacturing, a cleanroom is never a one-size-fits-all solution. Your process defines the parameters—airflow patterns, filtration efficiency, temperature stability, and vibration control—not a catalog of pre-engineered boxes. A custom turnkey cleanroom starts with your spec, then engineers every surface and system backward from that operational truth. The floor, often overlooked, becomes a material science problem: static-dissipative polymers, seamless chemical-resistant coatings, and load-rated substrates work together to eliminate particle generation at the source. Meanwhile, ISO Class compliance is designed in from day one, not bolted on as an afterthought. By treating classification as a measurable outcome rather than a vague promise, the build team removes guesswork and delivers a room that consistently hits target particle counts under real production loads.
The turnkey model also changes the economics. With a single contract covering design, construction, certification, and commissioning, there are no blame games between trades—one accountable entity owns the outcome. This integration shortens schedule, reduces change orders, and accelerates time-to-first-good-part. A custom cleanroom pays for itself faster than generic alternatives because it eliminates over-specification waste while avoiding the costly retrofits that plague off-the-shelf rooms. Ultimately, precision manufacturing demands more than just a clean room; it demands a controlled environment engineered as a production tool. Every material choice, every pressure cascade, every lighting fixture contributes to yield, repeatability, and operator safety. Custom turnkey delivery ensures that the cleanroom becomes an invisible enabler of your process, not a limiting constraint.
Contact Us
Contact Person: Amy Yang
Email: [email protected]
Tel/WhatsApp: 008619330882686
Website: https://www.genopharmatech.com/